As the owner and lead applications engineer at a 5-axis machining center supply company, I’ve spent 18 years on the shop floor and field troubleshooting calls where emergency stops (E-stops) made the difference between a minor setback and a catastrophic machine crash, part loss, or even personal injury. What surprises many new customers—our clients ranging from small job shops to large aerospace and medical device manufacturers—is that E-stop procedures on these complex 5-axis systems aren’t just a single big red button. They’re a layered, intentional workflow, built around the unique motion of 5-axis machines (which rotate and tilt cutting heads or workpieces across five axes, rather than the three linear axes of standard mills) to stop hazards fast while protecting the precision components that make these machines worth the investment. I’ve written this guide to walk through exactly what to do when that “oh no” moment hits—whether it’s a tool veering off-path, a workpiece slipping in a vice, or an operator’s glove catching on a spinning spindle. 5 Axis Machining Center
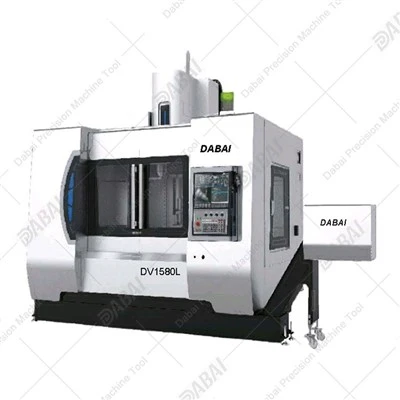
First, let’s start with the most critical rule I drill into every new customer during their on-site training: the first thing you do when a hazard is imminent is act on the closest E-stop device, no hesitation. That might sound basic, but 5-axis machines have E-stops placed strategically for a reason—there’s a top-of-machine pull-cord E-stop for overhead motion risks, a pendant-mounted E-stop for operators standing near the work envelope, and a stationery floor E-stop by the machine’s power cabinet, plus even a remote E-stop for line operators overseeing multiple machines. Why the closest? Every millisecond counts here, and fumbling for a button farther away wastes time that could let a spinning tool slice a workholding system, or a tilting rotary axis slam into the machine’s cast-iron frame. I’ll never forget a call last year from a medical parts shop where a new operator froze mid-tool change as their 5-axis machine’s B-axis (the tilt axis for the cutting head) started angling toward the vise’s clamps. They reached for the pendant E-stop instead of the floor E-stop at their feet, and by the time they pressed it, the B-axis had already dented the vise, chipped a carbide tool, and put a 2-week delay on a knee implant order. That’s the kind of small, avoidable misstep we’re here to prevent, so my first advice: skip the overthinking, grab the nearest E-stop first.
Once you’ve engaged the E-stop, the next step is to immediately isolate the machine’s power source to lock out motion. This is where 5-axis systems have a unique quirk that standard 3-axis mills don’t. On 3-axis machines, the E-stop usually cuts off spindle and axis power directly, but on 5-axis machines, the rotary axes (A, B, or C) often have hydraulic or pneumatic brakes that engage automatically when E-stop is pressed—but those brakes can sometimes release if power is cut completely incorrectly, letting a heavy workpiece or cutting head shift out of place. That’s why the correct second step is to flip the machine’s primary power disconnect switch (usually located on the side of the machine’s base, not a wall plug, which can be accidentally left on) and then unlock the main control cabinet to ensure all auxiliary power (for axis drives, spindle motors, and workholding hydraulics) is fully off. I always tell customers: never assume the E-stop alone is enough to hold a 150-pound rotary table with a titanium workpiece. We’ve engineered our 5-axis machines with redundant brake systems, but locking out power adds a second layer of safety that’s non-negotiable for post-hazard checks.
After the E-stop is engaged and power is locked out, you need to document the exact state of the machine to diagnose what caused the incident before you move anything. This is another step that’s often skipped in the chaos, but it’s critical for 5-axis machines because their five axes create a precise spatial profile. When an E-stop is triggered, the control system saves a snapshot of every axis position, spindle speed, workholding pressure, and even the G-code line that was running. Write that down, snap photos of the work envelope (checking for any contact between tool and workpiece, tool and machine structure, or workpiece and fixturing), and note if there was any unusual noise, alarm code, or error message on the control screen. I once had a customer run a second job without documenting a small E-stop trigger, and three months later, their control system threw a B-axis calibration error that traced back to an unreported collision from that initial incident. By the time they figured it out, they’d spent $12,000 on repairs and a whole week of downtime. Documentation isn’t just red tape—it’s your way to prevent repeating the same mistake with these complex systems.
Next, before you even think about clearing the E-stop or restarting the machine, you need to conduct a thorough, axis-specific hazard check. This is where 5-axis machines differ the most from standard mills, because their rotary axes can hide damage you can’t see at first glance. Let’s break this down axis by axis, since every 5-axis setup is either a head-tilt configuration (A and B axes on the cutting head, X, Y, Z linear) or a table-tilt configuration (A and B axes on the workpiece table). For head-tilt machines, start with the Z-axis (the main vertical axis) to make sure the spindle and tool are not hanging loose or at an angle that could fall once power is restored. Then move to the rotary axes: gently wiggle the B-axis manual knob (only once power is locked out) to check for excessive play in the tilt gears—unusual play here is a sign of a loose bolt or damaged bearing, which would cause a crash on the next run. For table-tilt machines, check the rotary table’s C-axis (the horizontal rotation axis) by rotating it slowly by hand (again, with power off) to make sure it doesn’t bind or jump. Also, never skip checking the workholding: 5-axis jobs use specialized vises or vacuum chucks, and a slip here can send a workpiece flying mid-motion. I always tell our customers to use a feeler gauge to check for gaps between the workpiece and fixture—any gap larger than 0.001 inches is a red flag, especially for tight-tolerance medical or aerospace parts.
Once you’ve confirmed all axes, fixturing, and components are free of visible or suspected damage, the next step is to clear the E-stop correctly. This is another area where I see mistakes happen all the time. You should never just twist the E-stop button back in and hit “cycle start”—that’s a recipe for a sudden, unexpected movement that could hit you or damage the machine. Instead, first turn the E-stop button clockwise until it pops back out (for push-pull style buttons, the most common on our machines), then turn the control system’s power key to the “on” position, wait 60 seconds for the control software and drives to initialize (5-axis systems take longer to boot because they have multiple axis drives), and then check the control screen for any active alarms—alarm code 420 (axis overtravel) or code 700 (rotary axis fault) are common after an E-stop. Only once all alarms are cleared should you perform a manual jog of each axis one at a time, at 10% of the machine’s maximum jog speed, to make sure it moves smoothly without binding or strange noises. If you jog all axes without any issues, then you can run a low-speed, air-only test (no tool engaged, no workpiece loaded) to confirm the spindle spins without vibration and all axes hold their position when commanded. I recommend this test every time after an E-stop, even a minor one—small issues with axis calibration can cause big problems when you’re cutting titanium or carbon fiber.
Finally, after resolving the immediate hazard, the most important step for long-term machine performance is to report and document the incident to your machine’s maintenance team (or your supplier’s service team, if it’s a new machine). Don’t try to hide a small E-stop incident—modern 5-axis machines have diagnostic logs that track every move, so covering it up just makes it harder to fix issues later. We have a team of field service engineers who can be on-site at most North American shops within 24 hours, and we work closely with customers to walk through E-stop procedures during initial training, plus offer annual refreshers because shop staff turnover is common. We also include a 24/7 emergency support line with every machine we sell, because even small shops can have an E-stop incident at 2 a.m. on a weekend, when the team is running a rush order.

I’ll wrap this up with a quick truth: 5-axis machining centers are powerful, precise, and expensive tools, but their complexity means E-stop procedures can’t be taken lightly. Every button, every axis, every lockout step is designed to protect both your investment and the people working around the machine. If you’re in the market for a new 5-axis machine, or you want to refresh your team’s E-stop training, don’t hesitate to reach out. We’ve built our business on supporting shops of all sizes, from startups with one machine to aerospace firms with 20+ 5-axis systems, and our team knows these machines inside and out, from the E-stop buttons to the rotary axis brakes.
Vertical Machining Center References
- National Institute for Occupational Safety and Health (NIOSH). Machinery Safety Guidelines for Computer Numerical Control (CNC) Machines. 2021.
- International Organization for Standardization (ISO). ISO 10218-1:2011, Robots for Industrial Environments – Safety Requirements – Part 1: Robot.
- Precision Machining Technologies Association (PMTA). 5-Axis Machining Best Practices Manual. 2022.
- Machine Builders Association (MBA). Emergency Stop Protocols for Multi-Axis CNC Machine Tools. 2020.
Dabai Precision Machine Tool (Jiangsu) Co., Ltd.
As one of the most professional 5 axis machining center manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy advanced 5 axis machining center for sale here from our factory. We also accept customized orders.
Address: No. 66-1, Zhenhu North Road, Hudai Town, Binhu District, Wuxi City
E-mail: elaine@dabaicnc.com
WebSite: https://www.cnc-dabai.com/
