If you’ve ever walked through a snack factory, a cosmetic bottling line, or a shipping distribution center, the smooth, consistent flow of boxes, pouches, and cartons hitting pallets doesn’t happen by accident. As someone who’s spent 18 years working in packaging industry production equipment—first as a field service tech, then running my own equipment supply team—I’ve seen too many new facility owners skip the deep dive on operation procedures, only to deal with unplanned downtime, product waste, or safety incidents that could’ve been avoided with clear, structured processes. Today, I’m breaking down the step-by-step operation procedures for our core equipment lines, the reasoning behind each step, and how our team supports customers every step of the way. I’m not here to sell you a one-size-fits-all machine; I’m here to walk you through how these lines work, so you can make informed choices for your operation. Packaging Industry Production Equipment
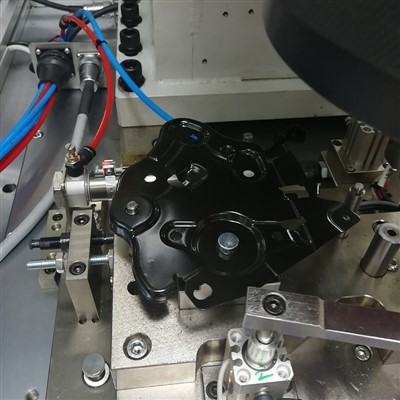
Pre-Operation: The Non-Negotiable Check You Can’t Skip (And Why We Train Your Team On This)
Before any button is pressed or conveyor starts moving, 90% of equipment issues start here. Too many new operators jump straight to testing the line, assuming the last shift’s team did a full check, and that’s when jams, misaligned parts, or even safety hazards pop up. We structure our pre-operation procedure in four non-negotiable steps, which we roll into every customer’s on-site training (no, it’s not just a 2-hour video—our techs spend 3 full days on the floor with your team, practicing hands-on checks).
First, we do a perimeter safety sweep. Every machine line has interlocks on guarding around moving parts, conveyor take-up points, and cutter heads. Our team trains operators to test each interlock manually: tug on a guarding door, hit the emergency stop button at every station, and confirm that all safety light curtains (the invisible beams that stop the line if something breaks) are calibrated. Last year, a craft cookie bakery we worked with had a near-miss when a new operator skipped this step and leaned over a conveyor to unjam a stack of dough sheets—they didn’t realize one interlock was broken, and the line moved when they reached in. This is non-negotiable because OSHA data shows 60% of packaging equipment injuries come from untested safety interlocks, per 2023 workplace safety stats.
Second, we do material and component verification. This sounds simple, but mismatched packaging materials are a top cause of downtime. For example, a vertical form-fill-seal (VFFS) machine—our most popular machine for snack pouches—requires film that’s the correct thickness, surface finish, and roll core size. If an operator uses a film roll meant for 10g candy pouches on a line set for 50g protein bars, the heat seal won’t stick, leading to leaks. Our check here includes matching part numbers for film, cartons, or lids to the line’s programmed specifications, and doing a 1-foot test run of film to check for wrinkles or tears that could cause jams. We also confirm that change parts (like different cutters for pouch sizes) are correctly installed—something a lot of new teams mix up when switching product runs.
Third, we calibrate the control panel and line sensors. Every packaging line has dozens of sensors: photoelectric sensors that detect if a pouch is in place, load cells that measure product weight for accurate filling, and temperature sensors for heat seals. Before starting, we walk the team through checking these: waving a small object in front of photoelectric sensors to confirm they trigger, testing load cells with a known weight to ensure fill accuracy, and verifying heat seal temperature is set to the film manufacturer’s recommendation (usually 120-180°C, depending on plastic type). Last quarter, a coffee roaster we supply had their line down for 4 hours because a sensor that detects empty pouches was out of calibration—they kept filling empty bags, wasting 1,200 pounds of coffee. We fixed that during a post-training follow-up, and now their team calibrates sensors every morning as part of their routine.
Fourth, we run a 5-minute dry test with no product or packaging material. This is the step that most new operators skip, but it’s critical. The line runs empty, simulating the full cycle of every station: film unwinds, forms a pouch, the filler moves, the seal jaws close, and the cutting blade triggers. Operators watch for misaligned film, uneven seal pressure, or any unusual noises (grinds, clunks) that signal a part is off. We teach teams to log any issues here instead of waiting for product to go through—saving both material and time.
The Production Run: Step-by-Step Line Execution, With Our Support Team Standing By
Once pre-operation checks are done, the production run starts, but it’s not just “push start and walk away.” There’s a structured sequence, and our team provides real-time support to adjust as you go, because no two production runs are identical—even for the same product.
First, line startup and initial pacing. We program each line to start at 50% of its maximum speed for the first 100 units. Why? If there’s a small misalignment, moving too fast will make it worse, leading to jams or damage. Once the first 100 units pass inspection (we have a smart sampling tool that checks seal integrity and weight in real time), operators can bump speed up to their target. For a standard VFFS line, that might be 60 pouches per minute; for a case erector that builds shipping boxes, it’s 12 cases per minute. Our techs leave a dedicated emergency contact for the first 30 days of the line being in full use, so if the first speed bump causes a seal failure or a jam, our team is on site within 24 hours.
Second, in-process monitoring and adjustment. During production, operators follow a 15-minute check routine, but we also recommend that our customers use our line’s built-in data tracking tool. This tool logs seal temperature, fill weight, line speed, and downtime events, so you can spot trends—like if seal temperature drops after 2 hours of run time, which might mean the heater is losing power. Last year, a pharmaceutical client we work with uses this tool to catch a faulty heater element on a blister pack line before it caused a batch of 50,000 pills to be sealed incorrectly. The line stopped automatically when the seal temperature dropped below FDA requirements, so no product was wasted.
A big part of our operation procedure is teaching operators to respond to small issues before they become big ones. For example, a minor film jam that’s only 2 inches long can be fixed by stopping the line, pulling the film free, and running a 1-foot test—instead of hitting the reset button and letting the jam worsen, which can break a cutter or tear a $500 film roll. We run role-playing drills during training, where our techs simulate common issues, so operators get comfortable solving them without waiting for a service call.
Third, mid-run changeover procedures. For companies that run multiple products in a day (say, a snack maker that does granola bars in the morning and rice cakes in the afternoon), changeover is the most time-consuming part of the run—bad changeovers can add 2+ hours of downtime. We’ve standardized our changeover procedure to take under 30 minutes for most lines, which is 50% faster than the industry average. The steps here include: stopping the line at a pre-designated parking point, locking out all energy sources (like power and air pressure) to prevent accidental movement, removing old change parts (cutter, seal jaws), installing new parts, re-calibrating sensors for the new product, running a 50-unit test, and doing a full safety check before restarting. We also provide color-coded kits for change parts, so operators never mix up a cutter for a 20g pouch with a cutter for a 50g one—something that used to cause a lot of delays before our team implemented this system.
Post-Production: Shutdown, Cleaning, and Documentation (Critical For Long-Term Equipment Life)
The end of the production run isn’t just hitting the stop button—it’s the step that keeps your equipment running for 10+ years, instead of needing a major overhaul in 3. We structure our post-operation procedure in three key steps, tailored for different line types (liquid filling, case packing, blister packaging, etc.).
First, controlled shutdown. Operators aren’t told to hit stop and walk away. We teach them to run the line empty for 2 minutes at the end of a run, so any residual product (like leftover sauce in a filling line) is flushed out, not left to dry and clog the system. For a powder filling line, this means running a small amount of cleaning agent through the filler nozzle to prevent clogs. We also make sure that all moving parts are in a safe position (like seal jaws closed, conveyor stops) before locking out energy sources.
Second, cleaning and preventive maintenance checks. This is where our team’s support continues—we provide a free cleaning schedule for every line, with step-by-step guides for each station. For example, a VFFS line requires daily cleaning of the film guide rollers, weekly cleaning of the seal jaws (using a non-abrasive pad to avoid scratching), and monthly lubrication of conveyor chains. We also include a quick check for wear and tear: looking for frayed belts, loose bolts, or worn sensors that need replacement. Last year, a food distributor we work with skipped the monthly chain lubrication, which led to a chain snapping mid-production, costing them $12,000 in lost product and downtime. We adjusted their maintenance schedule and now send a field tech every quarter to do these checks, so small issues are caught before they cause major damage.
Third, documentation and handoff. Every operator logs the run: how many units were produced, any issues that came up, maintenance done, and material used. This log is critical for traceability, especially for food and pharmaceutical companies that need to meet regulatory requirements (FDA, FSMA, etc.). We also provide a digital dashboard for customers, so they can access these logs from anywhere, track equipment performance over time, and schedule preventive maintenance before problems arise.
As a supplier, I don’t just sell you a machine and then disappear. Every step of these procedures—pre-operation, production run, post-production—is backed by our training, on-site support, and a 24/7 help desk that answers questions at 2 a.m. when your line goes down during a critical order. I’ve worked with small startups that are running their first packaging line, as well as Fortune 500 companies with 20+ lines across the country, and the biggest mistake I see is customers not taking the time to formalize these steps. It’s not about overcomplicating operations—it’s about reducing downtime, cutting product waste, and keeping your team safe.
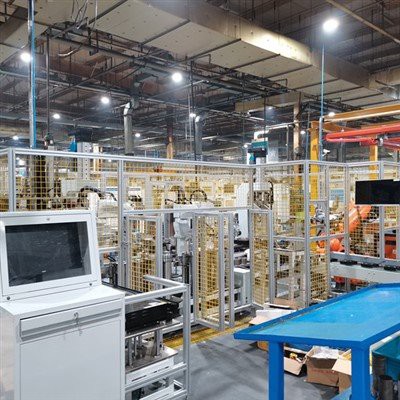
If you’re ready to streamline your packaging line procedures, upgrade your equipment, or just have questions about how these steps would work for your specific product, I’m here to help. Reach out to our team to schedule a no-obligation walkthrough and consultation for your facility.
References
Automotive Industry Production Equipment Occupational Safety and Health Administration. (2023). Workplace Injuries in Packaging and Goods Production. U.S. Department of Labor.
Packaging Machinery Manufacturers Institute. (2022). Standard Operation Procedures for Packaging Production Lines. PMMI Publications.
Food and Drug Administration. (2021). Compliance Guidelines for Packaging Equipment in Food and Pharmaceutical Facilities. FDA Center for Food Safety and Applied Nutrition.
Shanghai Zenyan Automation Engineering Co., Ltd.
As one of the leading packaging industry production equipment manufacturers in China, we warmly welcome you to buy advanced packaging industry production equipment made in China here from our factory. All customized machines are with high quality and low price. Contact us for quotation.
Address: 3rd Floor, Building A, No.5629 Beisong Road, Chedun Town, Songjiang District, Shanghai, China
E-mail: zenyan_sh@163.com
WebSite: https://www.zenyanauto.com/
